Best ABS 3D Printer: Enclosed Models Compared
12 min
- What ABS Demands from a Printer
- Three Tiers of 3D Printers for ABS
- Best ABS 3D Printers at a Glance
- Specs That Matter More Than Marketing
- The Economics: Is an ABS-Capable Printer Worth Buying?
- When a Print Service Beats Buying
- Getting ABS Prints Right
- FAQ about Best ABS 3D Printer
- Match the Machine to ABS
Key Takeaways
- Every enclosed printer can claim to print ABS; the machines that do it reliably share four specs: a hot end with headroom past 250°C, a bed above 90°C, a real enclosure — and, for large parts or dense print schedules, a chamber that actively holds its heat.
- Chamber temperature is not chamber existence: an enclosure blocks drafts, a passive chamber warms from the bed, and only an actively heated chamber holds a set temperature. No chamber figure on the spec sheet means treat it as passive.
- Hot-end headroom is a selection practice, not a law: leave 20–30°C of margin above your working temperature where practical, and follow the printer manufacturer's limits.
- The economics go by volume: occasional ABS rarely justifies a new machine — and if your parts face heat or impact that ABS itself cannot handle, the material ladder, not the printer, is the upgrade.
- For production ABS without the hardware investment, a print service with engineering FDM runs it on tuned machines with engineer review — worth a quote whenever volume is low or consistency matters.
Materials decide machines. ABS typically wants a 230–250°C hot end, a 90–110°C bed, and an enclosure that keeps cooling drafts away from shrinking layers — formulation-dependent numbers, so the filament datasheet has the final word. This guide to choosing the best ABS 3D printer turns those demands into a shopping checklist: the specs that actually matter, the three tiers of machines that can do the job, and the honest economics of when buying a 3D printer for ABS filament beats sending the file out. If you are still deciding between materials, our ABS vs PLA and ABS vs PC comparisons sort that first.
What ABS Demands from a Printer
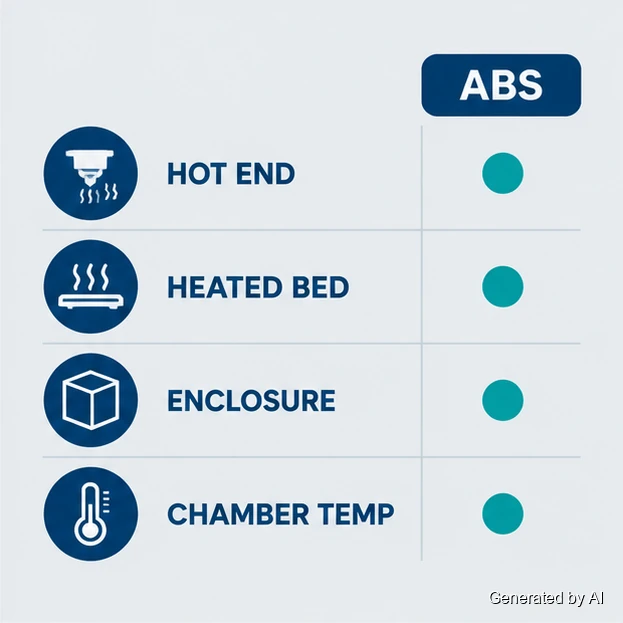
The shopping list writes itself from the material's temperature behavior (the full framework is in our ABS temperature resistance guide; here it becomes hardware):
| Machine spec | ABS needs (typical, formulation-dependent) |
|---|---|
| Hot end | 230–250°C working range — buy headroom past it |
| Heated bed | 90–110°C |
| Enclosure | Strongly advised (warp control) |
| Chamber temperature | Warm, draft-free, and stable |
Treat these as common working ranges, not universal requirements — the filament datasheet is the authority, and brands differ (Prusa, for one, lists 255°C for its ABS). The mechanism behind the table is short: ABS shrinks as each layer cools, and shrinking layers pull parts into warp; a warm, still chamber slows that cooling and lets each layer settle before stress builds. PC simply moves every threshold up — if that filament is on your list too, the upgrade route is covered at the end of this page.
One line in this table eliminates more ABS 3D printer candidates than the rest combined: the hot end. A machine specced to 260°C has no headroom for ABS's working range plus growth, and running any hot end at its own ceiling all day trades reliability for nothing.
Three Tiers of 3D Printers for ABS
Machine classes, not model numbers, are the honest way to shop — models change yearly, classes change slowly. The specs cited below were checked against manufacturer documentation in October 2026; brands revise without renaming, so confirm the current spec sheet before buying.
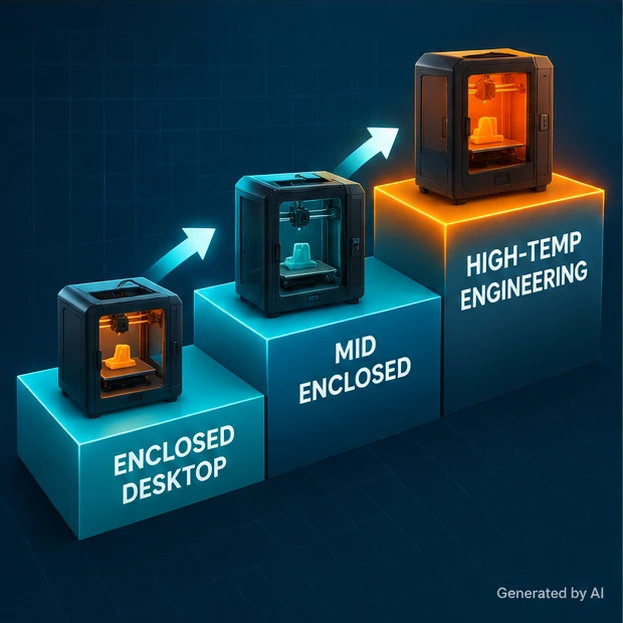
Tier 1 — Enclosed desktop (the working default). Fully shrouded consumer machines with ~300°C-rated hot ends: Creality's K1C (220×220×250mm, 300°C hot end, 100°C bed) and Bambu Lab's P2S (256×256×256mm, 300°C hot end, 110°C bed, chamber sealing up to 50°C). They hold drafts out and bed heat in well enough to print ABS reliably, and they are what most people mean by "a printer that can do ABS." Their ceiling: the chamber is passive (warmed by the bed and the heat of printing, not actively heated), so large parts and dense print schedules push them to their best.
Tier 2 — Mid-range enclosed with active chamber control. Machines that add active chamber heating to the desktop format: Qidi's X-Plus 3 (280×280×270mm, 300°C hot end, 120°C bed, independent 65°C chamber heating). ABS becomes boringly reliable here — the machine stops being part of the quality equation.
Tier 3 — Fully enclosed high-temp engineering machines. The future-proof tier: hot ends rated 350°C and beyond, actively heated chambers holding real chamber temperatures. Qidi's X-Max 3 (325×325×315mm, 350°C hot end, 120°C bed, 65°C active chamber), Bambu Lab's H2S (340×320×340mm, 350°C hot end, 120°C bed, 65°C active chamber), and Intamsys's Funmat HT line all play here. For pure ABS these are performance overkill — but if PC or engineering materials are on your roadmap, they buy the headroom once instead of twice.
A few honest boundaries inside the tiers. Tier-1 machines printing large, dense ABS parts are running at their best but with no margin for growth; Tier-2 active chambers narrow that gap; and every tier assumes you run the checklist (dried filament, tuned profiles, closed door): the hardware enables good ABS prints, it does not automate them.
Best ABS 3D Printers at a Glance
Five machines that cover the three tiers, with the four numbers that decide ABS capability:
| Printer | Build volume | Max nozzle | Max bed | Chamber |
|---|---|---|---|---|
| Creality K1C | 220×220×250 | 300°C | 100°C | Enclosed, passive |
| Bambu Lab P2S | 256×256×256 | 300°C | 110°C | Enclosed, passive (up to 50°C) |
| QIDI X-Plus 3 | 280×280×270 | 300°C | 120°C | Actively heated, 65°C |
| QIDI X-Max 3 | 325×325×315 | 350°C | 120°C | Actively heated, 65°C |
| Bambu Lab H2S | 340×320×340 | 350°C | 120°C | Actively heated, 65°C |
Match the row to your part: small brackets and housings sit fine in the passive rows; large parts, batch consistency, or engineering-filament plans are what the active-chamber rows are for.
Specs That Matter More Than Marketing
Within any tier, four details separate machines that hold ABS to spec from machines that merely survive it:
Chamber temperature vs chamber existence. Three levels matter here: an enclosure blocks drafts and may retain some heat; a passive chamber warms up from the bed and the print itself; an actively heated chamber has a dedicated heater with real temperature control. The spec that counts is a chamber temperature reading — an active heater, or at minimum a sensor showing what the chamber actually reaches. "Fully enclosed" with no chamber figure tells you it is a windbreak that holds whatever heat the bed gives off, nothing more. Bambu Lab's own FAQ confirms the P2S has no active chamber heating — it regulates chamber temperature through the enclosed chamber and an airflow flap — so an enclosed badge alone says nothing about chamber temperature.
Hot-end headroom. A common selection practice: pick a hot end whose rated maximum sits above the filament's recommended printing temperature, leaving 20–30°C of margin where practical, and follow the printer manufacturer's limits. A 300°C-rated hot end prints ABS comfortably; one running at its own ceiling all day leaves no room for formulation differences or the occasional hotter job.
Bed surface at temperature. ABS wants aggressive adhesion at 90–110°C and clean release at cool-down; PEI-type surfaces handle this well, and bare glass tends not to. Check what the machine ships with and what the bed actually reaches at the corners, not just the center.
Filtration and venting. ABS printing produces odor and some airborne emissions; a recirculating carbon/HEPA filter and an exhaust port are useful specs — NIOSH's 3D-printing safety guidance treats enclosure design, exhaust airflow, and make-up air as a system, so a filter alone does not make any room safe. Neither affects part quality; both affect where the machine is allowed to live, and the printer and filament makers' safety instructions come first.
The Economics: Is an ABS-Capable Printer Worth Buying?
The price gap between an open printer and a properly enclosed one is, in effect, the admission ticket for ABS. Whether the ticket pays back is a volume question:
| Your situation | Sensible move |
|---|---|
| Mostly PLA/PETG, occasional curiosity about ABS | Do not buy for it — the ticket outweighs the use |
| Regular ABS parts | Tier 1–2 machine; the machine pays for itself |
| Large batches with dimensional requirements | Tier 2 — consistency is what you are paying for |
| First printer | Start with PLA-friendly open machines; beginners should not start here |
A simple framework for the comparison: estimated in-house cost per usable part ≈ machine cost allocation + material + failed prints + labor + maintenance + ventilation. Without real numbers for your volume and failure rate, treat any blanket claim — cheaper to buy, cheaper to outsource — as an assumption, not a fact. The honest adjustment is failure rate: ABS prints fail more often on marginal setups, and each failed print is filament, electricity, and an evening. A well-configured Tier-1 machine prints ABS at high success rates, which is why the machine ticket usually pays back before the material savings do.
When a Print Service Beats Buying
For most people shopping this category, the real question is not which machine but whether the machine is needed at all. A service is the shorter path when print volume is low, when parts need consistent quality across batches, or when you would rather skip the drying, enclosure, and tuning checklist entirely.
JLC3DP prints ABS via FDM on production machines with tuned profiles, and the settings and chamber discipline are built in, and an engineer reviews every uploaded model before production. For ABS parts with dimensional requirements or batch consistency needs, upload the model for an instant quote and compare the per-part number against the machine budget.
Getting ABS Prints Right
Whichever machine you choose, the failure modes are the same four, and the countermeasures are known:
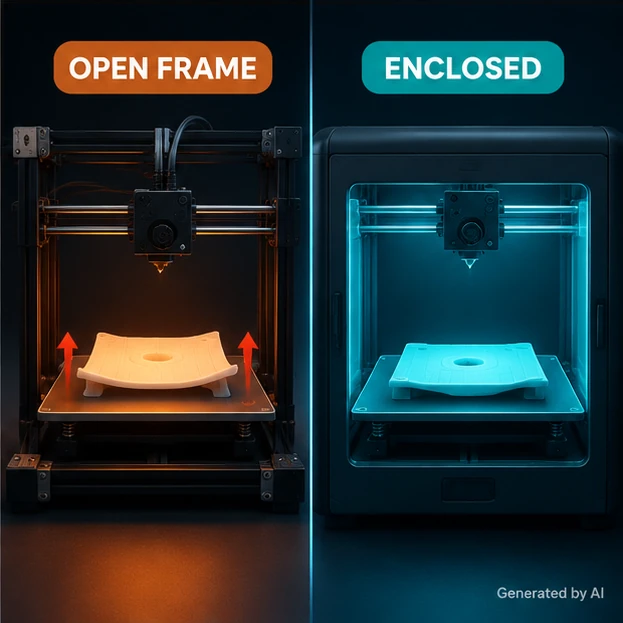
- Warping, the classic ABS failure: shrinking layers curl corners off the bed. Countermeasures in priority order: heated bed, brim, enclosure. An open machine skips all three and pays for it.
- Layer splitting, usually a sign of low chamber temperature or a hot end running at the bottom of its range. Raise chamber warmth first, nozzle temperature second.
- Wet filament symptoms (popping, stringing, weak layers): ABS absorbs moisture and wet spools betray it. Dry before printing; store sealed.
- Poor surface finish, typically print speed or cooling fan settings fighting the material: slow down, close the fan, and re-test.
One upgrade worth knowing about: annealing a finished ABS part near (but below) its glass transition relaxes internal stresses and improves heat deflection — useful when a part needs extra thermal margin. The trade-off is dimensional (annealed parts shrink), so test first.
FAQ about Best ABS 3D Printer
Q: Can any 3D printer print ABS?
No — an open-frame machine fighting cooling drafts produces warped, layer-split ABS parts more often than good ones. A heated, enclosed chamber is the practical minimum, which is what puts ABS a tier above PLA in hardware terms.
Q: What temperature do I need to print ABS?
Common ABS settings run a 230–250°C hot end and a 90–110°C bed, but the filament datasheet is the authority — formulations differ. Printing heat is not service heat: the finished part's own limit is around 85–95°C deflection, far below the printing temperature.
Q: Do I need an enclosed printer for ABS?
Strongly advised, yes. ABS warps as shrinking layers pull corners off the bed, and an enclosure that holds warmth is the difference between a flat part and a curled one. The mechanism and the countermeasures are the same story covered in our ABS vs PLA comparison.
Q: Is a 300°C hot end enough for ABS?
It can be, if the hot end reaches your filament's recommended settings within the printer's rated limits. A maximum temperature is not a recommended everyday operating temperature — follow the printer and filament manufacturers' instructions rather than a universal margin rule.
Q: Does ABS require an actively heated chamber?
No single chamber setup is right for every ABS print. An enclosure reduces drafts and retains heat; active chamber heating adds control for larger parts, dense schedules, or engineering-filament plans. Whether it is needed depends on the filament, the part geometry, and the printer.
Q: How much should I spend to print ABS reliably?
A Tier-1 enclosed machine carries ABS reliably without exotic spending. Spend further only when volume justifies it: the machine's price divided by your realistic ABS part count is the honest per-part cost to compare against a print service's quote.
Q: Can a print service print ABS for me?
Yes — services that list ABS as an FDM material run it on production machines; JLC3DP prints ABS with tuned profiles, manufacturability checks, and engineer review. It fits when print volume, batch consistency, or part requirements make buying hardware questionable.
Match the Machine to ABS
The order of operations saves money: read ABS's temperature demands first, the machine's spec sheet second, and the four discriminating specs (chamber temperature, hot-end headroom, bed surface, filtration) before the badge. Tier 1 covers ABS handsomely; spend further only when volume or PC-grade plans justify it. Buy the ticket only when the rides justify it, and when they do not, the upload is one step away.
Keep Learning
Best ABS 3D Printer: Enclosed Models Compared
Key Takeaways Every enclosed printer can claim to print ABS; the machines that do it reliably share four specs: a hot end with headroom past 250°C, a bed above 90°C, a real enclosure — and, for large parts or dense print schedules, a chamber that actively holds its heat. Chamber temperature is not chamber existence: an enclosure blocks drafts, a passive chamber warms from the bed, and only an actively heated chamber holds a set temperature. No chamber figure on the spec sheet means treat it as passive......
How Much Does 3D Printing Cost? A Complete Breakdown
We get this question a lot at JLC3DP: “How much does 3D printing cost?” And here’s the truth: Some projects can be surprisingly cheap, while others cost more than you’d expect. There’s a myth floating around that 3D printing is basically free once you own a printer. (If only it were that simple, right?) The reality is, whether you’re printing at home or outsourcing to a service like ours, the cost depends on a handful of important factors, machine type, materials, design complexity, and even how much ......
Top 5 3D Printer Tables of 2026: Boosting Your 3D Printing Experience
Choosing the right table for your 3D printer that enhances printing stability, reduces noise, and provides organized storage space is important for achieving high-quality prints and optimizing your workflow. In this guide, we'll look at what makes a good 3D printer table and recommend the best 3D printer tables on the market in 2026. Below are our top five 3D printer tables and stands for 2026, highlighting their features, benefits, and why they might be perfect for your printing space. Best 3D Printe......
Recommended Best Resin 3D Printers in 2024
In recent years, resin 3D printers have developed rapidly in the home 3D printer market. Compared with traditional FDM printing, resin printers can provide higher precision and more delicate printing details. The improvement of printing technology allows users to easily complete the production of high-precision models at home. This article will recommend several of the most competitive resin 3D printers in the 3D printing market in 2024 to help you choose the most suitable equipment and the factors to......
How Much is a 3D Printer? A Comprehensive Guide for Every Budget
3D printing is becoming more and more popular, bringing countless creative and practical possibilities. So how much is a 3D printer? 3D printers have a very wide price range, depending on the printing process, materials, and complexity of the 3D printing solution. This article will analyze the cost of 3D printers based on their type and intended use, helping you find a model that fits your budget. Types of 3D Printers and Their Costs 1. Entry-level 3D Printers ($100 - $500) Entry-level 3D printers are......
Best 3D Printers for Beginners
Embarking on your journey into the world of 3D printing can be both exciting and daunting. With a plethora of options available, choosing the right 3D printer as a beginner is crucial for a smooth transition into additive manufacturing. To simplify your decision-making process, we've curated a list of the top 10 beginner-friendly 3D printers that offer a perfect balance of affordability, ease of use, and quality output. Creality Ender 3 V2 Neo Price: $379.00 Features: Full-metal integrated design, CR ......